Quality from die trial to stamped-part delivery
Quality & inspection planning
A stamping quality plan connects the die trial, approved sample, and repeat batch. WenXinDa reviews material condition, formed dimensions, burr direction, functional fit, and finish against the released drawing. The same requirements guide tooling corrections, production checks, and the records needed at receiving.
01 Define acceptance
Critical features
A hole pattern must locate the bracket; a clip must fit without damage; a formed tab must sit correctly after springback. Define these functional relationships alongside burr limits, visible faces, and measurement condition, then connect each check to the released drawing.
- Identify the dimensions and surfaces that control fit, function, and safety.
- Use a common datum setup and measurement condition.
- Check affected features at the right stage, including after finishing.
- Give dimensional and cosmetic requirements their own acceptance criteria.
02 Evidence
Inspection records
A useful report identifies the part revision, tool or trial reference, material, sample, and measured result. Agree the documentation needed for die approval separately from the records supplied with production batches, including any first-article or customer-specific submission.
| Requirement | What the check covers | Supporting record |
|---|---|---|
| Material identification | Specified alloy and condition, with the material identification and traceability level required for the order. | Material documentation and lot references included in the order scope. |
| Dimensional inspection | Drawing characteristics, nominal values, tolerance limits, measurement methods, and sample identity. | Report identifying part number, revision, sample, and measured results. |
| Die-trial approval | Trial parts checked for formed geometry, burr condition, function, and tool corrections against the current drawing. | Trial reference, dimensional results, open-action list, and written sample disposition. |
| First-article review | A new or revised part checked against the production drawing before the next release stage. | First-article report and approval record in the agreed format. |
| Visual & finish checks | Visible faces, edge condition, color, texture, and the specified surface treatment. | Agreed visual checklist, photographs, or finish documentation. |
| Special measurement or submission | Measurement of complex geometry, external testing, or a customer-specific submission package. | A defined measurement or submission plan with the required report format. |
03 First article
Trial sample approval
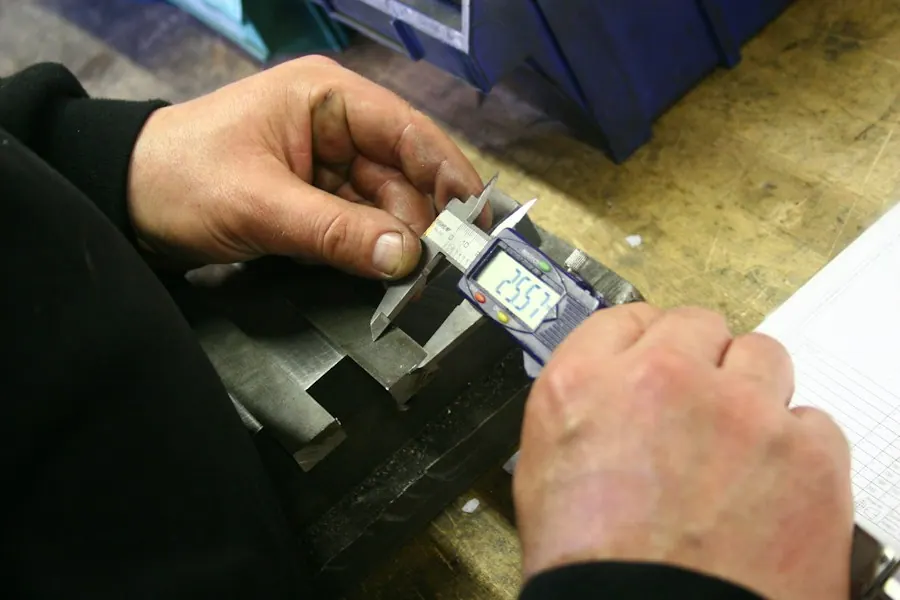
Trial samples show how the die and production material work together. Review formed dimensions, springback, edge condition, and assembly fit before approving the next release. Record the trial material and tool revision so corrections, repeat trials, and production samples can be compared on the same basis.
- 01
Confirm the revision
Align the drawing, CAD, material, finish, and customer specifications. Resolve conflicting requirements before the sample is made.
- 02
Define the inspection plan
Number the agreed characteristics and set datum fixtures, free-state or restrained measurement, sample quantity, and the report template.
- 03
Review measured results
Compare the sample with the specified limits. Record exceptions with feature references and measured values.
- 04
Record the disposition
Identify any corrective action, repeat inspection, or buyer-authorized deviation. State who can approve the release.
- 05
Define repeat-order controls
Agree what triggers a new sample review: material or temper changes, die repair, replaced inserts, tooling changes, or a new drawing revision.
04 Receiving checks
Incoming inspection
Clear labels, comparable measurements, and an organized document package reduce avoidable questions at receiving. We connect these delivery details with the quality plan so your team can identify and review parts efficiently.
Part identification
Keep part number, drawing revision, batch reference, and quantity visible in the agreed pack or carton labels.
Comparable measurements
Use the same datums, measurement method, and part condition at production and receiving to make results comparable.
Exception handling
Provide a direct route for reporting a discrepancy, with the drawing requirement, measured result, affected quantity, and supporting photos.
What inspection is included?
Can we use our inspection template?
Are material certificates available?
How are special inspection requirements handled?
How should a discrepancy be reported?
06 Control by stage
Inspection stages
Material variation, die setup, punch wear, forming, and finishing can each affect a stamped part. Place checks at the stages where they can reveal the change, and agree when a tool correction or material change needs a new approval.
| Stage | Purpose | Control focus |
|---|---|---|
| Incoming material | Verify the specified material and condition against the order before it enters production. | Material designation, condition, documentation, and batch identity. |
| Setup / first piece | Check the initial setup against the current revision before a longer run. | Die and material identity, feed or setup references, first-piece dimensions, edge condition, and release. |
| In process | Watch features affected by tool wear, forming variation, or a changed setup. | Features affected by tool wear, setup changes, and forming variation. |
| After finishing | Assess features altered by coating, heat treatment, deburring, or assembly. | Finished dimensions, masked surfaces, appearance, and assembly fit. |
| Before dispatch | Match quantity, identity, records, and packaging to the approved order. | Part identity, quantity, inspection records, and protective packing. |
07 Reading a report
Dimensional reports
An inspection report should be easy to read against the drawing. Feature numbers connect each result to a requirement; sample and lot references identify the parts checked. Actual values make the record useful for engineering review as well as receiving acceptance.
A clear dimensional report includes
- Part number, revision, material, lot or batch identity, and the sample inspected.
- The feature number and nominal requirement, including limits or geometric control.
- The actual measured value, units, and the measurement method or fixture.
- Whether the result applies before or after finishing, in the free state, or in a defined inspection fixture.
- The decision for an out-of-limit result and the person authorized to approve a deviation.
For a formed bracket, spring clip, plated contact, or assembly position, specify the datum setup and measurement condition before trial samples are made. The tolerances guide explains how to mark these requirements in the drawing.
08 Exceptions and changes
Nonconformance and corrective action
When a result falls outside an agreed limit, the next step is to establish the affected scope and contain the parts. The decision then follows the function of the feature and the order requirements, with reinspection after any corrective work.
- 01
Identify the scope
Record the feature, measured result, drawing limit, batch identity, and quantities potentially affected.
- 02
Contain the parts
Separate suspect product from approved product while the measurement and production history are reviewed.
- 03
Agree a disposition
Discuss rework, replacement, use-as-is approval, or another action against the order and functional risk.
- 04
Verify and close
Record the approval, repeat measurement where needed, and any control change for later releases.
Changes stay tied to the part record. Drawing revisions, material changes, and tooling adjustments are reviewed for their effect on fit, finish, and the need for a new sample approval.
Approval that matches the application
Functional checks
A long inspection report is useful only when it checks the right characteristics. Start with the function of the component, then connect each critical feature to a method, sample, and approval decision.
Locating bracket
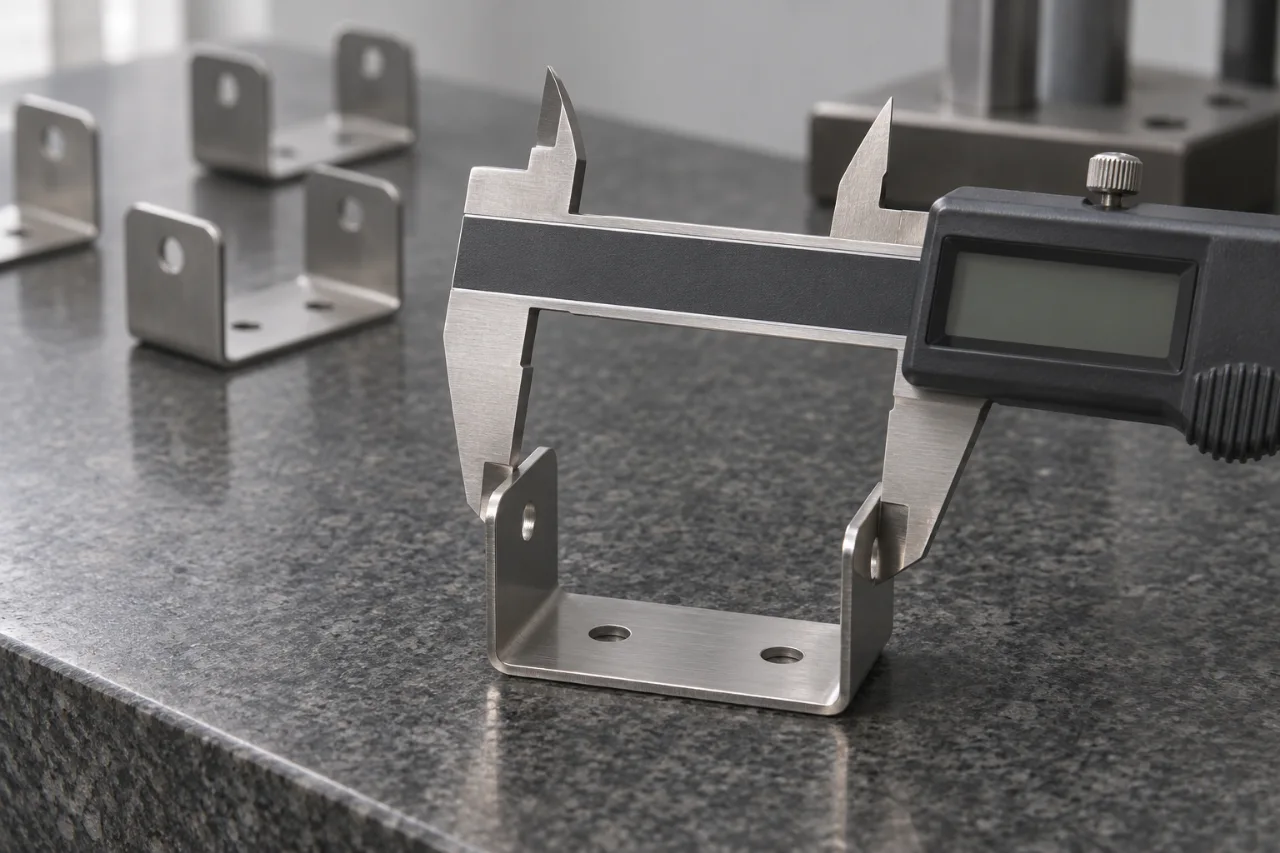
Check the hole pattern from the mounting datums and the formed condition used in assembly. Review flange height, angle, and any locating feature after the specified finish. If a checking fixture is part of the plan, define how the part is located and restrained before comparing the readings.
Spring or retaining clip
Combine dimensional checks with the agreed functional condition. Free-state geometry and the geometry under a working deflection answer different questions. Tie material grade, temper, burr orientation, and trial identity to the sample so a repeat order can follow the same approved specification.
Plated electrical contact
Keep contact areas, edge condition, plating requirements, and permitted handling marks visible in the inspection scope. Identify the stage at which dimensions are checked and the records associated with the finish. Packaging should preserve the surfaces that were accepted during release.
Cosmetic formed cover
Define the visible faces and the approved finish reference. Separate cosmetic criteria from assembly fits and hidden surfaces. Include the inspection viewing condition and protective packing where appearance matters, so acceptance follows a shared reference from sample review to receiving.
Send your ballooned drawing or existing inspection template with the RFQ. Mark the characteristics that can stop assembly, affect the working interface, or trigger a receiving hold. We can then review the inspection scope with the tooling and manufacturing route, rather than leaving quality requirements to the final shipment.
Next step
Request a quote
Send the drawing and any quality checklist. We will help connect critical features, inspection records, and delivery approval in one clear scope.