Core capabilities · Metal stamping & die development
Metal stamping and tooling
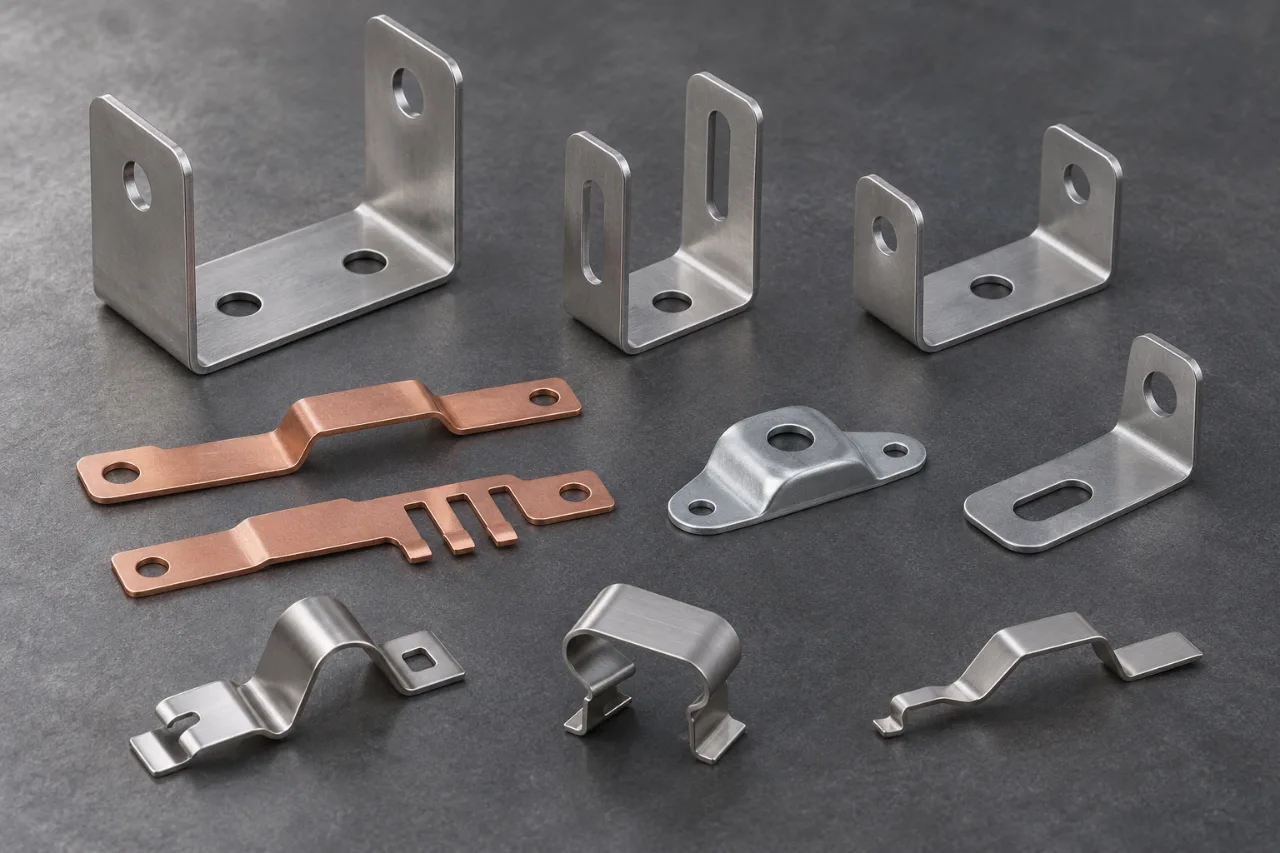
Metal stamping and stamping die development are the focus of WenXinDa. We support OEM brackets, clips, contacts and formed components from drawing review and tooling development through die trials, sample approval and repeat production. Material, strip layout, forming, finish and inspection are planned together, with secondary machining considered where the finished part requires it.
A punch and die cut and form sheet or strip into repeated components. Tooling links the material, feature sequence and production demand to a consistent finished part.
Start with the part function, then choose the operations that create its working features.
Metal stamping
A defined die development scope
Connect the die concept, included operations, trial deliverables and ownership terms before tooling begins.
Trial parts with approval criteria
Check the critical dimensions, formed features, edge condition and assembly fit against the agreed part revision.
A controlled production baseline
Carry the approved sample, material condition, finish and inspection requirements into repeat releases.
01 Scope
Practical manufacturing support for your parts
A good part brings together the right material, an efficient manufacturing route and a finish that suits its working environment. These are the details we connect during project review.
01
Stamping die development
Review the part geometry, strip or blank layout, cutting and forming sequence, and access to wear components. Match the tool concept to the design and expected demand.
02
Custom stamped components
Specify brackets, clips, contacts and formed hardware around their function. Material grade, temper, thickness and burr direction belong beside the finished dimensions.
03
Trial to repeat production
Use die trials to resolve the part and tool together. Agree corrections, sample approval and production checks before releasing regular orders.
Custom stamped parts built around their assembly function
The part function guides the stamping route. A clip must retain, a contact must conduct, and a bracket must locate correctly after forming. We review the controlled drawing, material condition, critical features and expected demand before defining the tooling project.
Part family
Why stamping may fit
Key question before tooling
Clip or retention spring
A repeatable cut and formed profile from strip.
What material temper, spring function, and edge orientation are required?
Electrical contact or shield
Thin conductive material with repeated openings and formed tabs.
Which areas carry current, need plating, or must remain uncoated?
Mounting bracket
Piercing and forming can be combined in a controlled sequence.
Which holes and flanges control assembly, and what may change in the next revision?
Washer, shim, or simple blank
High repetition of a flat profile can justify dedicated cutting tooling.
Do nesting, material utilization, and required edge quality support the tool investment?
A part family is a useful starting point; its function, material and lifetime demand guide the tooling decision.
Choose the die concept before committing to tooling
Pilot tools, stage tools and progressive dies serve different development and production needs. Review the forming sequence, material yield, handling and future revisions alongside the demand forecast. The first sample quantity alone is not enough to choose a die.
Approach
Best when
Trade-off
Pilot / bridge tooling
Trial parts or design learning are needed before the production route is fixed.
Compare the initial tool scope with handling and recurring part cost.
Progressive dies
A stable part and recurring demand justify a connected strip sequence.
Assess die investment, strip yield, trial work and wear-component care.
Stage tooling
Separate cutting or forming stages suit the part and release pattern.
Account for transfer, part location and inspection between operations.
Strip layout connects material yield, part orientation and the sequence of cutting and forming operations.
Plan the finish with the stamping route. Plating, coating and deburring can change contact surfaces, mating dimensions and edge condition. Mark the surfaces that carry current, touch a seal or fit another part so those functions are protected.
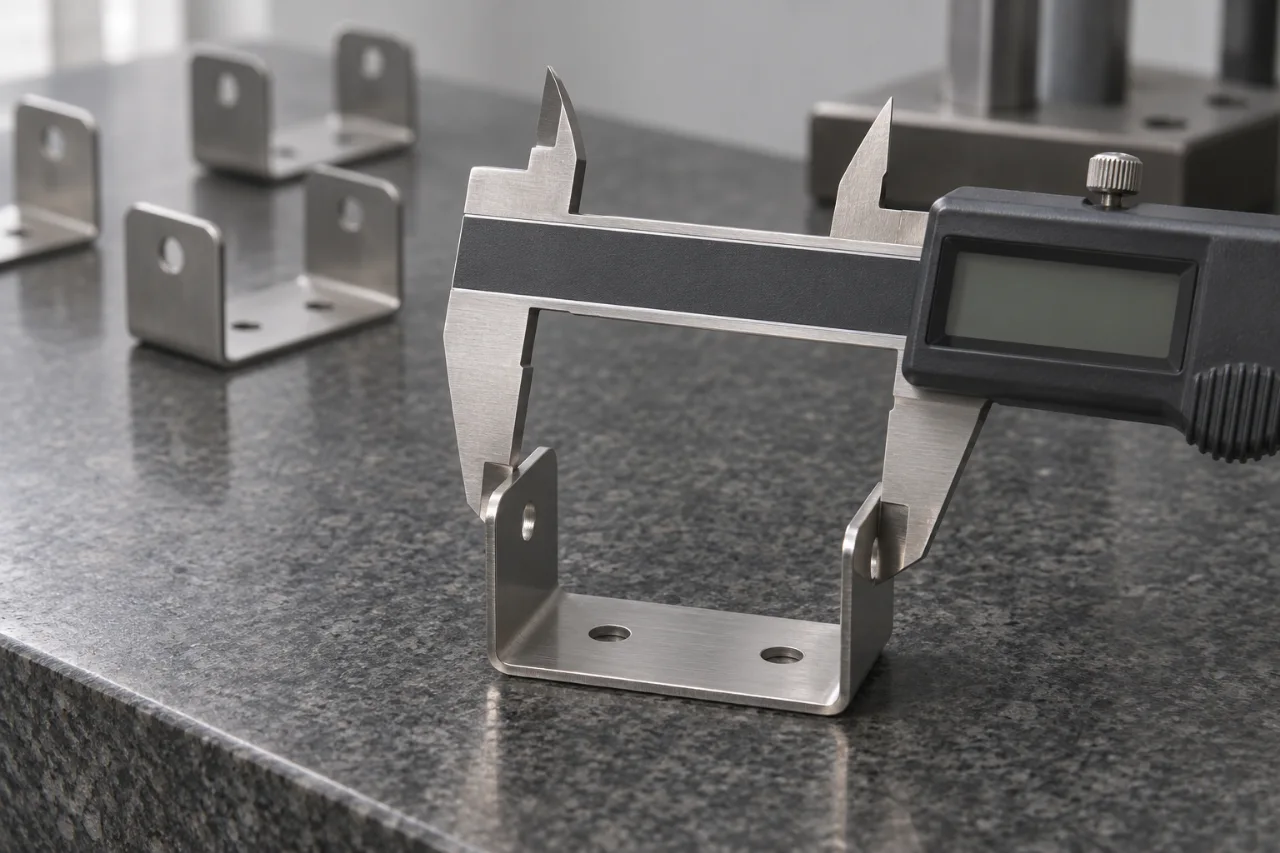
Checking a formed feature against the part specification
Material and strip condition shape the die
The die is designed around the specified material, not a generic sheet label. Thickness variation, temper, grain direction, coating, and surface finish can change forming force, springback, burr condition, and the final part shape.
Material input
Why it matters in stamping
Specify in the RFQ
Steel or stainless strip
Strength, forming response, and corrosion protection affect the route.
Grade, condition, thickness, finish, and any post-form heat treatment.
Aluminum strip
Temper and grain orientation can influence bending and cosmetic appearance.
Alloy, temper, grain or appearance direction, and coating or anodizing needs.
Copper alloy strip
Conductivity and spring performance can depend on alloy and condition.
Exact alloy, condition, contact surfaces, and plating specification.
Pre-coated material
Cut edges and formed corners may expose or damage the supplied finish.
Coating standard, protected faces, and any required edge treatment.
Approve any proposed material substitution before the strip layout and die details are frozen.
Die condition, locating features and maintenance affect the consistency of repeated stamped parts.Process detail
Define the die project and the production it supports
Treat the die as a project with deliverables, approval points and continuing responsibilities. Separate its one-time investment from the recurring part price. A tooling proposal should identify what is included, what the trial will establish and what the buyer will receive at production release.
Project element
Define in the proposal
Decision for the buyer
Die design and construction
Die concept, operations, material specification and included fixtures or gauges.
Does the scope cover the complete approved part?
Trials and corrections
Trial material, sample quantity, inspection results and correction responsibilities.
What result must be accepted before production release?
Ownership and ongoing care
Physical assets, design files, storage, service and transfer arrangements.
How will repeat orders and future tool changes be controlled?
Agree die ownership, storage, maintenance, expected life, and revision responsibility before commissioning tooling.
Design features to review before die construction
Stamping DFM turns the drawing into a workable strip and forming sequence. A feature that looks minor in CAD can change tool construction, waste, or the number of operations. Identify functional dimensions first, then review the surrounding geometry.
Feature
Tooling concern
Buyer decision to make
Hole close to an edge or bend
A narrow web may distort or leave limited support for piercing.
Which hole location is critical, and can the surrounding profile change?
Tight inside corner
The punch or die corner can wear and concentrate stress.
Is the sharp corner functional, or can a radius be accepted?
Short flange or small tab
Forming access and springback can affect the final position.
What dimension controls assembly, and which face is the datum?
Wide flat area
Residual stress can affect flatness and appearance.
How flat must the part be in its installed condition?
Required burr direction
The cut edge has a direction that can affect handling or contact.
Which side faces a mating part, user, seal, or electrical contact?
Review DFM suggestions before die construction, when a radius, relief or feature-position change is easiest to make.
Tool approval and change control
A tooling quotation should explain what the die makes, which operations follow stamping, and what is supplied for approval. Define trial samples, the drawing revision used for the die, and the criteria for releasing repeat production.
Approval point
What to agree
Why it matters
Tool design review
Strip concept, critical datums, part orientation, and secondary operations.
Changes are easier to evaluate before steel is committed to the final die.
Trial sample
Sample quantity, material condition, finish state, and inspection report scope.
A trial part must represent the features and conditions being approved.
Production release
Accepted sample, controlled drawing revision, packaging, and order quantity.
The released baseline prevents a later order from being judged against different criteria.
Engineering change
Who approves revisions, pays for tool changes, and receives updated samples.
Even a small profile change can alter a punch, station, or inspection fixture.
Document die ownership, storage, access, and maintenance responsibilities in the commercial agreement.
Inspection after stamping and finishing
Define which attributes are checked on the first article and which are monitored during repeat production. Typical concerns include hole and flange position, formed angle, edge condition, appearance, and the dimensions of any post-machined features.
Plating, coating, deburring, and heat treatment can change the final condition. Show which dimensions apply before or after these steps and identify contact or mating surfaces that need masking. If an inspection report or material document is required with each shipment, state the scope and frequency before quotation.
Prepare a stamping RFQ that can be compared fairly
Provide the controlled PDF drawing and CAD model, material grade and condition, sheet thickness, finish, critical features, burr direction, trial quantity, annual forecast, and expected design life. Include the mating assembly or a short description of the part function.
Ask the quotation to separate tooling cost, trial scope, unit price, secondary operations, finish, inspection, packing, and shipping assumptions. If the design is still moving, disclose planned revisions so pilot tooling or a non-tooling route can be evaluated without comparing unlike scopes.
Plan the operations after the press
The pressed shape is sometimes only one step toward a usable part. Secondary operations should be identified before the die is designed so locating surfaces, part orientation, and handling can work across the full route.
Follow-on operation
Why it may be needed
Specify before tooling
Deburring or edge finishing
A handling, sealing, or contact edge has a defined burr limit.
Which edges matter, burr direction, and the final acceptance method.
Tapping or machining
A thread or mating face cannot be achieved in the stamped state alone.
Datum relationship between stamped and machined features.
Heat treatment
A required spring or wear condition is achieved after forming.
Material condition, final-property requirement, and inspection state.
Plating or coating
Corrosion, appearance, or electrical contact requirements need a final surface.
Coating standard, contact areas, masking, and dimensions after treatment.
Assembly or kitting
The stamped part ships with fasteners or as a subassembly.
Installed components, orientation, labeling, and protective packing.
The final part specification should cover every included operation, not just the die output.
Protect repeatability through the supply chain
For a repeat part, agree the approved drawing and material condition for each release, the scope of production checks, and how changes are communicated. Ask whether material certificates, sample records, or shipment-level inspection documents are required. These choices affect price and preparation, so they belong in the RFQ.
Packing is part of the specification when thin profiles can nest, tangle, or mark one another. State whether parts need separation, orientation, corrosion protection, or lot labels. Share the destination and delivery basis so the final quotation can distinguish manufacturing from transport responsibility.
From an assembly problem to a stronger stamping brief
A useful stamping project starts with the job the component performs. Tell us where the bracket locates, how the clip deflects or which terminal face carries current. Then connect that function to the material condition, formed geometry and final surface. This makes the tooling discussion more focused: the die is developed around a specific finished part, a measurable trial and a defined repeat-order requirement.
Project brief
Engineering review
What the buyer can approve
Mounting bracket with holes that must align after forming
Review hole-to-flange relationships, forming sequence and assembly datums together. Define whether the final coating is included in the accepted dimensions.
Trial parts checked in the formed and finished condition, with the critical mounting relationship identified in the report.
Spring clip with a specified working action
Connect alloy, temper, bend geometry and grain direction to the installed deflection and agreed force test.
A sample plan covering both free-state dimensions and the functional condition used by the assembly team.
Electrical contact with a functional plated surface
Identify contact faces, burr direction, plating specification and the areas that must remain clear.
The complete terminal condition, including geometry, surface requirements and packing that protects the contact faces.
Buy a production plan, not just a piece price
A competitive stamping proposal should show how the part moves from a released drawing to an approved die trial and then into repeat supply. Ask for the one-time tooling investment, trial deliverables and recurring part scope separately. Include secondary operations, finish, inspection and packing in the same comparison. This gives your team a clear basis for choosing between stage tooling, a progressive die and a flexible fabrication route.
Ready to review a part? Send the drawing with the current revision, material grade and temper, first release and forecast demand. Add the mating view, the functional issue your team wants resolved and the sample evidence needed for approval. We can then focus the discussion on the die concept and finished component that your next assembly build actually needs.
For repeat programs, send the annual forecast as well as the first order. It gives the tooling review a useful basis for balancing investment, piece cost and future revisions.
Application brief
Use the application, mating features and approval checks to turn a drawing into a clear manufacturing brief. Bring your part number and the assembly requirement that drives the design.
Brackets, contacts and formed sheet metal components
Industrial equipment / formed brackets
Stamped mounting bracket
A mounting bracket can look right on the bench and still hold up the assembly line. Hole position, bend angle and coating thickness all affect how it seats against the mating component. The project starts by identifying the mounting faces and the dimensions that control the fit, rather than treating every drawing dimension as equally important.
Engineering & inspection +
The objective is a bracket the receiving team can identify, inspect and move into assembly with a clear approval record. Send the mating details with your drawing to make the quotation more useful.
Engineering approach
Review the formed model with the mating arrangement. Establish functional datums, hole-to-bend relationships and the finished condition in which the part is measured.
Compare the stamping sequence with a cutting-and-bending route against the first order, repeat releases and expected drawing changes.
Plan the burr direction, accessible edges and surface protection together. Include any secondary holes or fasteners in the same supply scope.
Approval checkpoints
Check mounting-hole position from the agreed functional datums.
Approve formed height, angle and fit against the mating requirements.
Match finish, edge condition and packing to the released specification.
Clips, brackets, and reinforcements from pilot runs through steady production.
Industrial equipment
Wear plates, shims, and formed hardware for long service life.
Electronics & electrical
Shields, contacts, and stamped hardware where conductivity matters.
General metal OEM
Brackets, shims and formed hardware with a manufacturing route matched to their geometry and demand.
03 Finishing
Finishing & post-processing
Finishing protects the part and prepares it for use. Choose the treatment around corrosion, wear, appearance and contact surfaces, with masking and final dimensions planned from the start.
Option
What it does
Common use
Electroplate (Zn, Ni)
Corrosion and appearance on steel and copper alloys.
Indoor and mild outdoor exposure
Powder coat
Color and durability on stamped shapes.
Visible consumer or industrial parts
Deburr / tumble
Removes sharp edges for handling and assembly.
Before plating or coating
Explore the process
Explore the operation your part needs
See how each operation handles the geometry, material and assembly features in your design.
Stamping die development
Die scope, trials, sample approval, ownership and maintenance.
Start with the files you have and highlight the features that matter most. These four details help us connect your design to the manufacturing route and finished-part price.
01
Current revision
Provide the dimensioned drawing and available CAD with matching part number, revision, and units.
02
Material & finish
State the complete material specification, condition, finish requirements, and any permitted alternatives.
03
Critical features
Identify functional dimensions, datum features, cosmetic criteria, and required inspection records.
04
Quantity & delivery
Include release quantity, expected repeat demand, destination, and the required delivery date.
A useful tooling quote separates die design and build, trial samples, inspection, production part price and secondary work. It also records ownership, storage, maintenance and how a future drawing revision will be handled.
How are die trials different from a production release?
Die trials establish whether the tool and specified material can produce the required part. Trial results may lead to tooling corrections or a drawing clarification. A production release records the accepted sample, controlled revision, finish condition and inspection plan after those points are resolved.
What information is needed for export packing?
Send the destination, preferred Incoterm and named place, plus any labeling or document requirements. Thin clips and profiles may need separation to prevent tangling; finished steel parts may need corrosion protection during transit.
When is a progressive die worth considering?
A progressive die can be attractive when the shape is stable and repeat quantity can spread the tooling investment. Compare the complete forecast, die cost, material use, piece price, maintenance, and secondary work against a pilot or fabrication route.
What happens if the drawing changes after the die is built?
The change may require new punch or die components, an updated strip layout, or fresh approval samples. Agree who authorizes and pays for revisions before tooling is commissioned, and identify the controlled drawing revision for each trial.
Can a prototype be stamped before production tooling?
A pilot, stage, laser-cut, or fabricated route may provide evaluation parts before a full progressive die is justified. The prototype route should be identified in the quote because its edge condition and repeatability may differ from the intended production process.
Why specify burr direction?
A cut edge can have a burr on one side. If that edge contacts a user, seal, mating part, or electrical surface, its direction and acceptable condition should be shown on the drawing. Deburring requirements should be quoted with the part.
Does a stamping quote include the die and finishing?
Ask for separate line items or explicit inclusions. A complete comparison should show die design and build, trial approval, part price, secondary operations, finish, inspection records, and packing. The commercial terms should also state die ownership and maintenance responsibility.
How should I compare stamping with laser cutting?
Compare the same finished part over the same expected demand. Laser cutting can avoid a dedicated die during design changes; stamping may reduce repeat unit cost once the geometry and volume are stable. Include finishing, inspection, material yield, and change costs in both routes.
Next step
Let us help you move the part forward
Send your drawing with the material, quantity and target delivery date. Tell us where the part fits and what matters most, whether that is assembly, appearance, cost or repeat supply.